01
Load Analysis
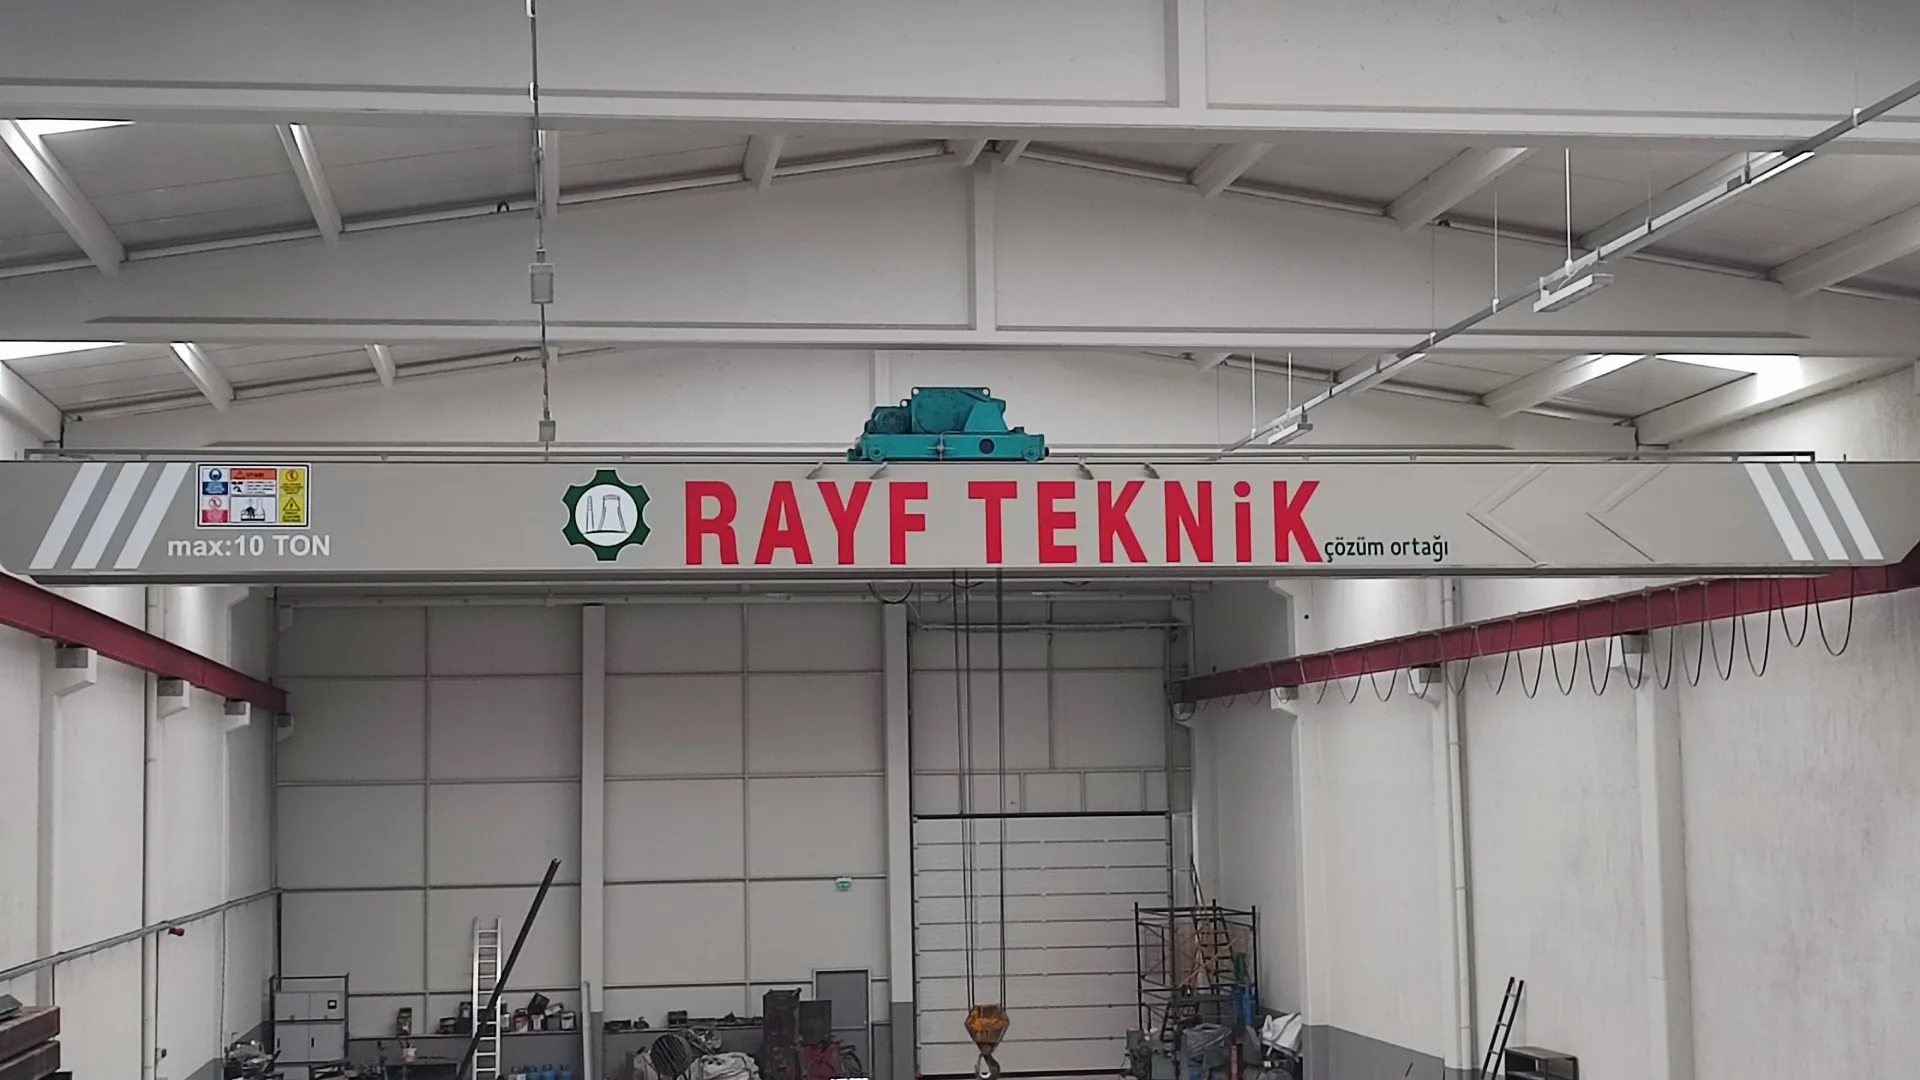
Capacity, span and duty class are defined during the gantry or overhead crane survey.
WORK PROCESS
Capacity, span and duty class are defined during the gantry or overhead crane survey.
Fabrication, rails and erection are written into the crane package.
Girders, wheels and anchorages are calculated for the lifting load.
The gantry or overhead crane is fabricated in the workshop.
Components are marked according to the erection sequence.
The crane is installed on its rails and load tested.
The test report and maintenance notes are handed over to the plant operator.
EXECUTION
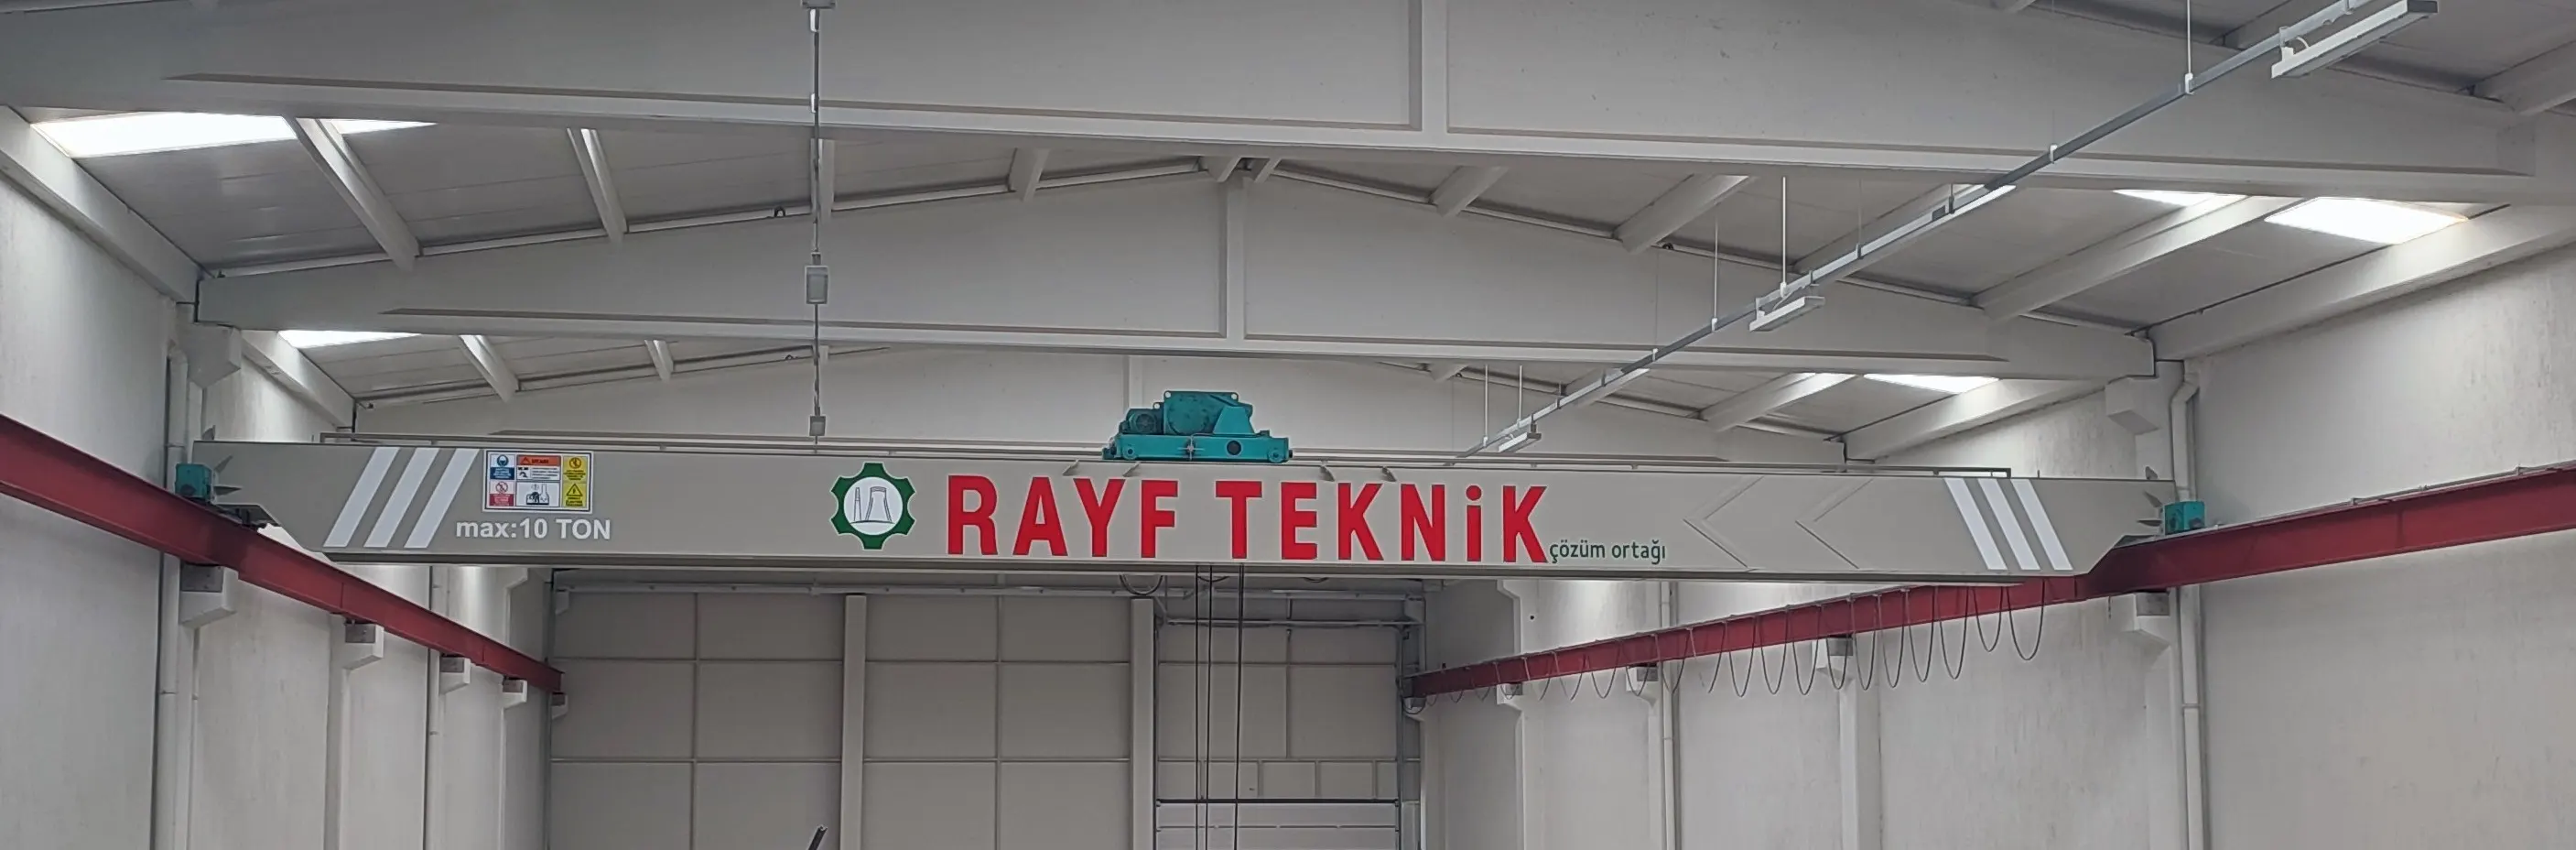
The choice between an overhead and a gantry crane is made according to the line and column layout. Floor-mounted cranes for chimney maintenance are assessed separately.
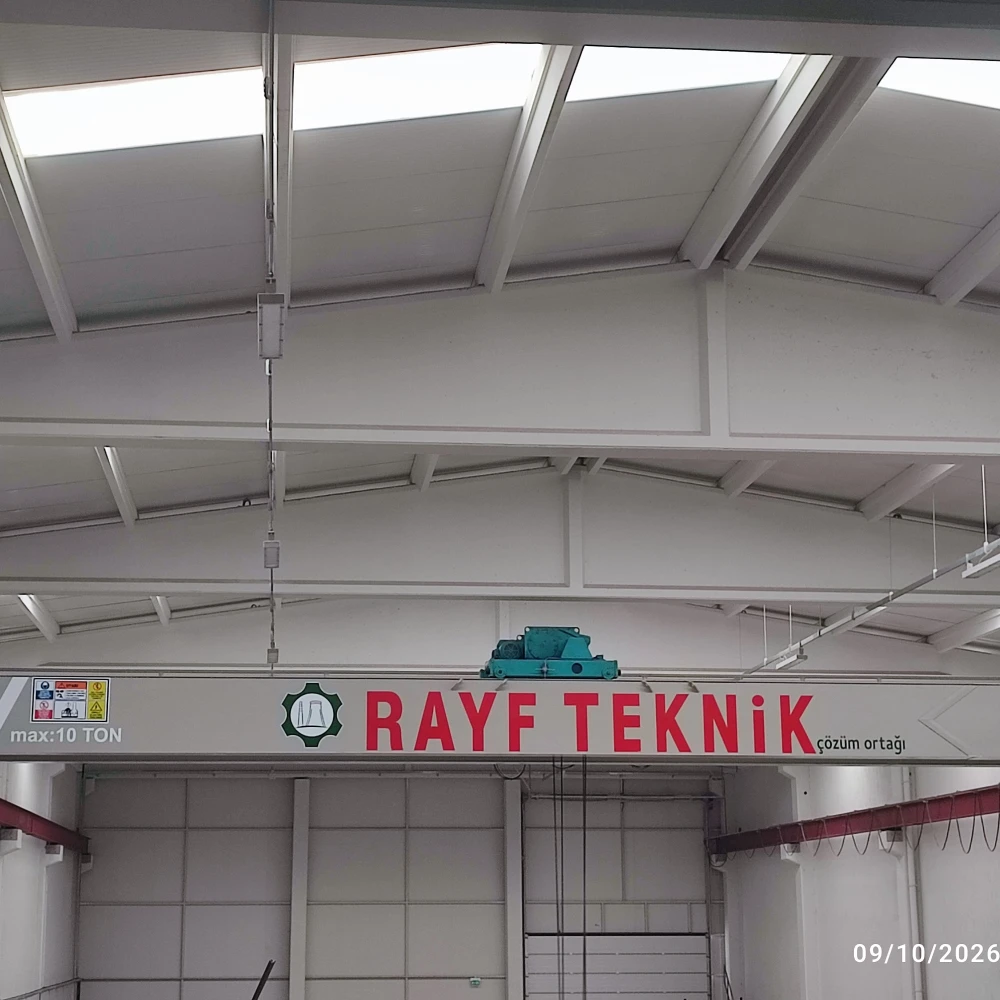
Rails, girders and anchorages are resolved in the same plan as the structural steel.
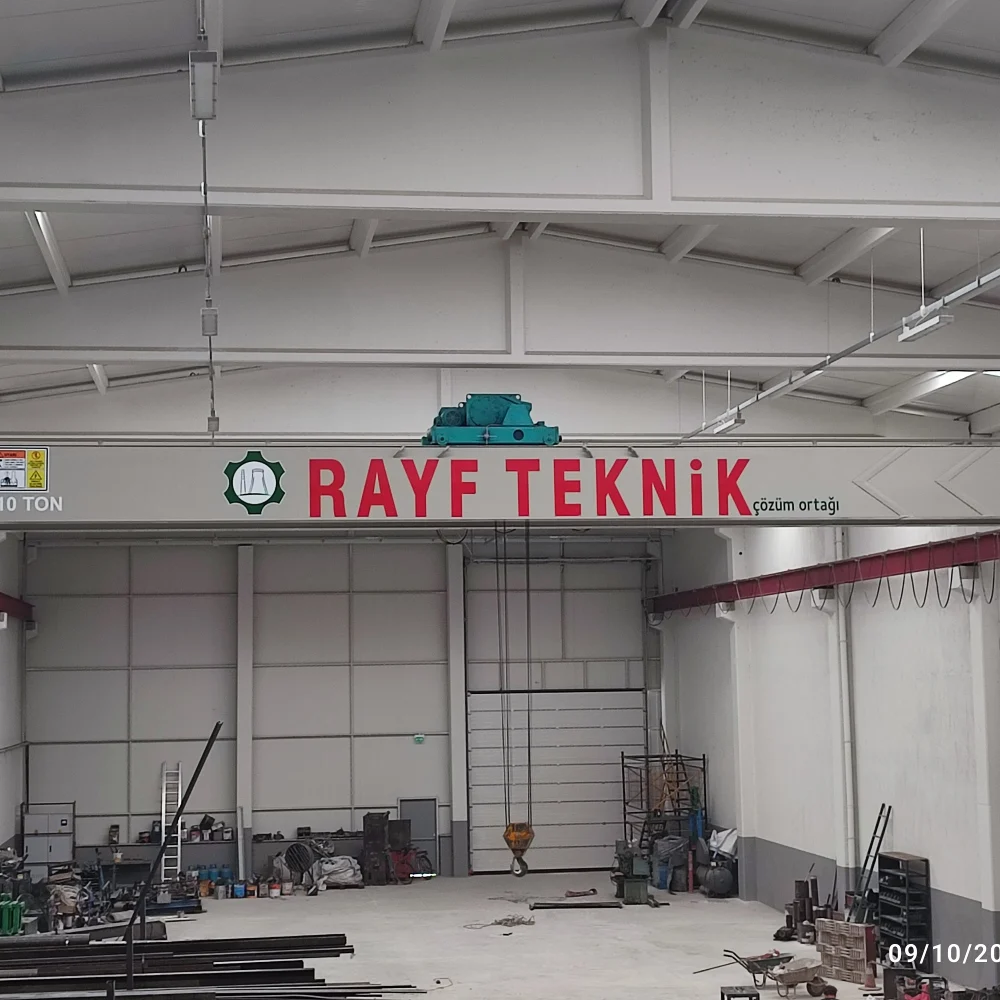
Erection is coordinated with the crane corridor. A load test record is provided at handover.
ABOUT THE SERVICE
Gantry and overhead crane systems are industrial lifting solutions used to move heavy or bulky loads in a controlled manner within production, maintenance and storage areas. The crane type is determined by the weight of the load, the working span, the lifting height, the frequency of operation and the geometry of the facility.
Overhead cranes generally travel on load-bearing columns and runway beams inside a production building. With gantry cranes, by contrast, the loads are transferred to the ground through the crane's own legs. As a result, the structural connections of the two systems, and the effects of their loads on the existing structure, can differ considerably.
In industrial crane projects, looking only at the capacity of the hoisting mechanism is not enough. Crane girders, rails, wheel loads, connecting elements, the power supply system and maintenance areas must all be assessed within the same design.
Rayf Teknik's experience in structural steel and tall industrial structures is a significant advantage when detailing the load-bearing structures to which crane systems are connected. In new facilities, the structural connections for crane runways can be built in while the reinforced-concrete and steel designs are being prepared.
Where heavy equipment is to be attached to reinforced-concrete structures built by the slipform method – such as silos, industrial chimneys or process towers – the necessary embedded plates and structural anchorages must be prepared during construction. Designing these details in advance, rather than creating new connection points in the concrete after the slipform has risen, allows much more controlled work.
Slipform technology is not a crane system, nor is it a direct part of crane manufacturing. On large industrial projects, however, the two disciplines can work hand in hand on the same site. Particularly where process equipment must be lifted to high elevations or heavy components moved during plant maintenance, the lifting systems need to be compatible with the structural design.
Preparing the structural steel members used in crane manufacture to the correct dimensions, executing welds and connections in line with the design, and precisely aligning the rail axes during erection all have a direct impact on operating performance.
On gantry and overhead crane projects, Rayf Teknik aims to develop engineering solutions tailored to the facility's existing structure, the load to be lifted and the intended use. Drawing on its site experience in structural steel, reinforced concrete and slipform construction, the company treats a crane not merely as a machine but as a handling system that works together with the structure it is connected to.
A well-planned crane system streamlines production flow while allowing maintenance and heavy-lift operations to be carried out in a more orderly way.
TECHNICAL SPECIFICATIONS
The capacity of gantry, overhead and floor-mounted cranes is selected according to line span and hoisting class. The rows below show a typical fabrication and erection framework.
TECHNICAL ADVANTAGES
Cranes make lifting safe and well planned on chimney and steelwork sites. The advantages are illustrated with site photographs.
Gantry, overhead or floor-mounted cranes are selected to suit the job.
01
Gantry, overhead or floor-mounted cranes are selected to suit the job.
SERVICE GALLERY
OTHER SERVICES
 View Details ↗
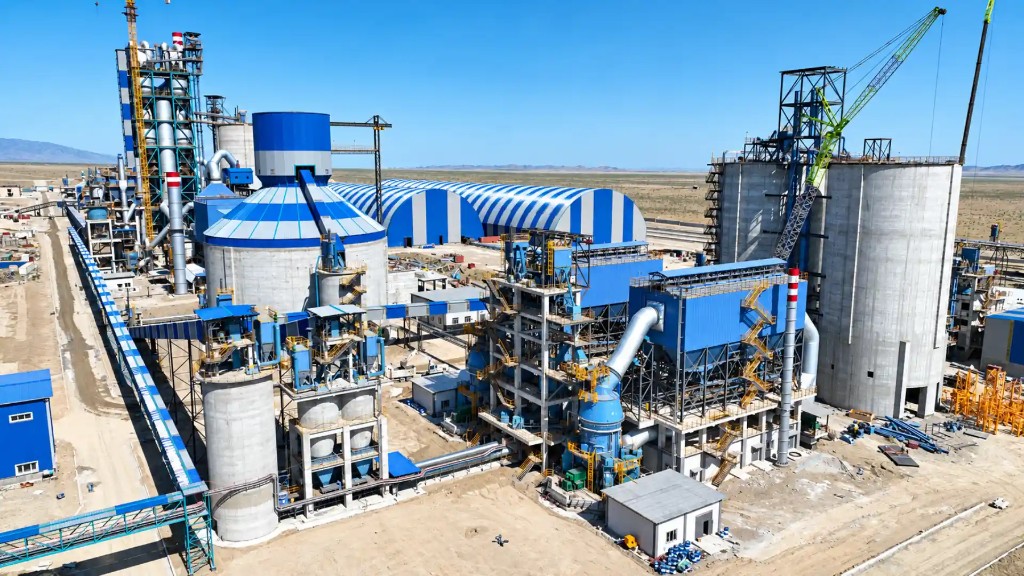
Seza Yapı — Seydişehir road construction site
Structural steel delivers high load-bearing capacity for platforms, galleries and production buildings. It is also used to support equipment lines connected to reinforced-concrete structures.
 View Details ↗
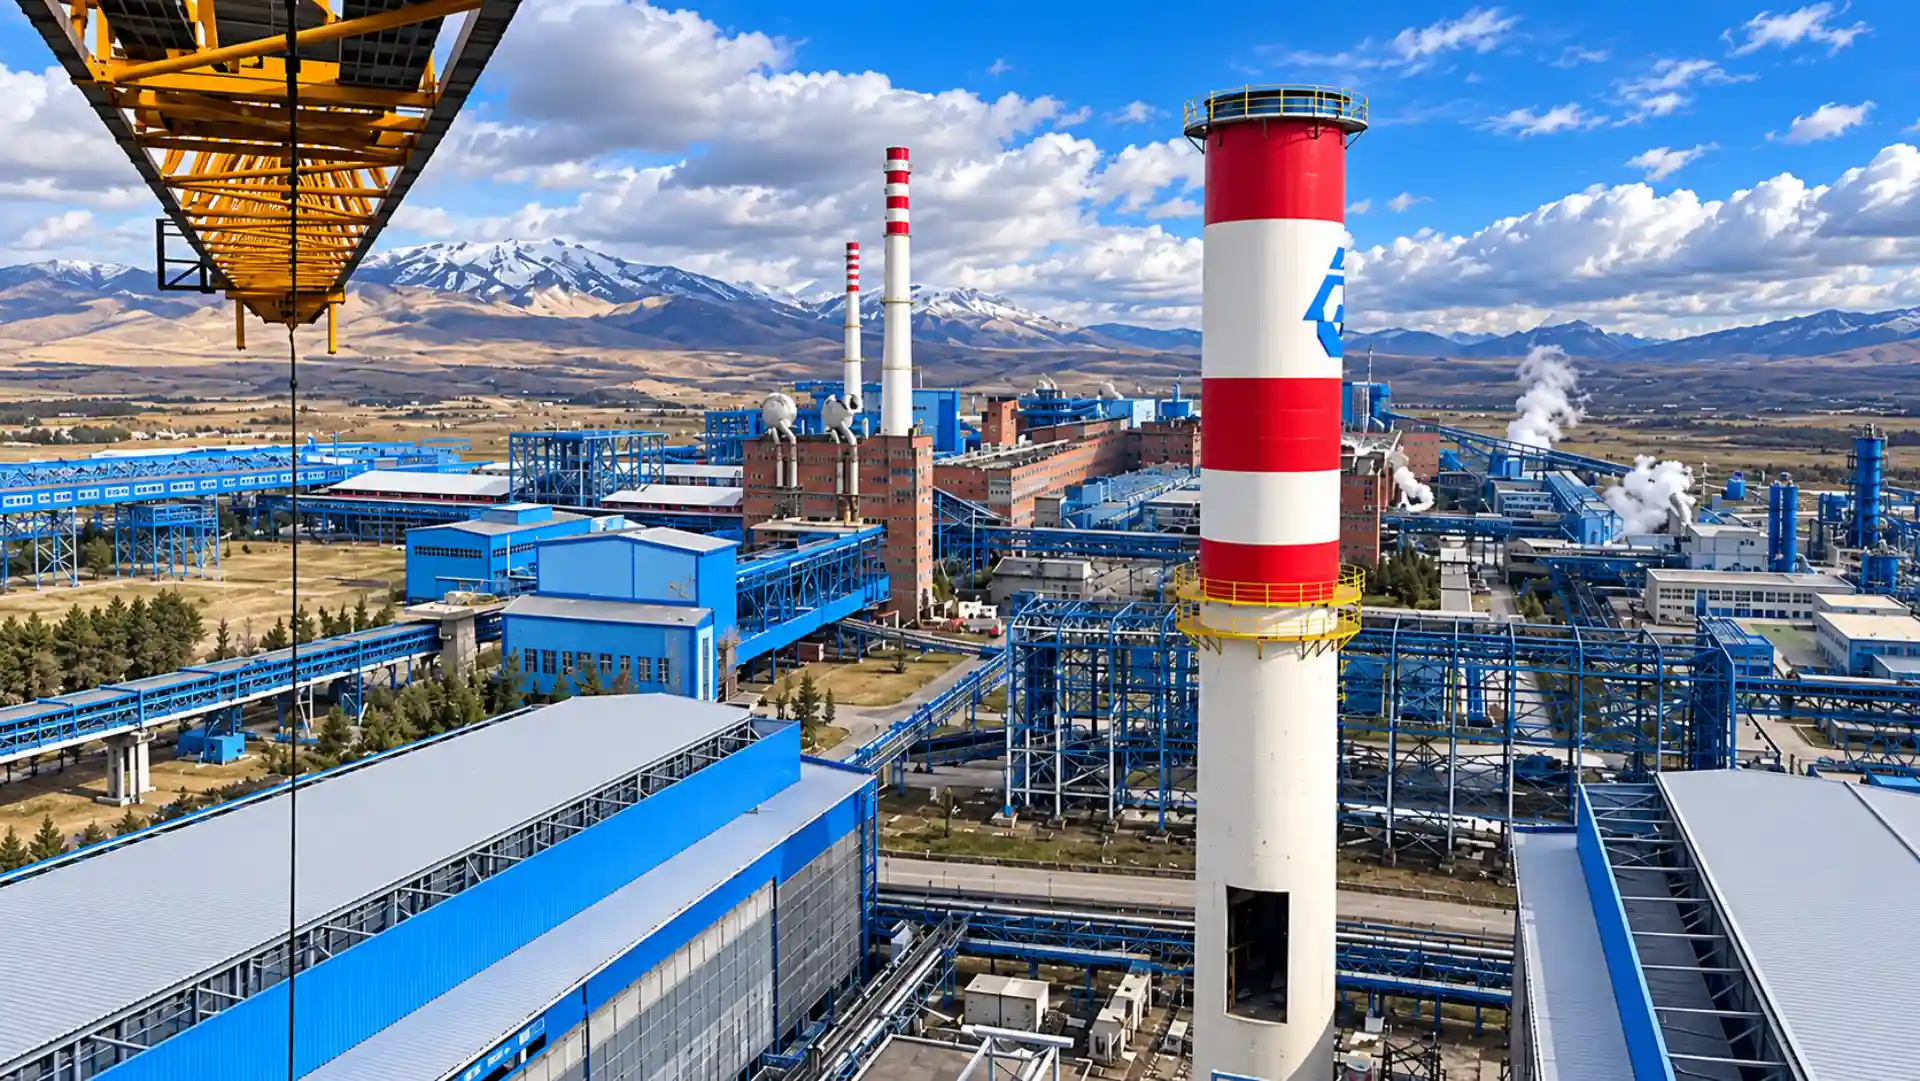
Ilgın / Konya — cement plant
Silo slipforming allows tall reinforced-concrete silos to be built in one continuous pour. Concreting, reinforcement fixing and hydraulic lifting advance together in a single coordinated production cycle.
 View Details ↗
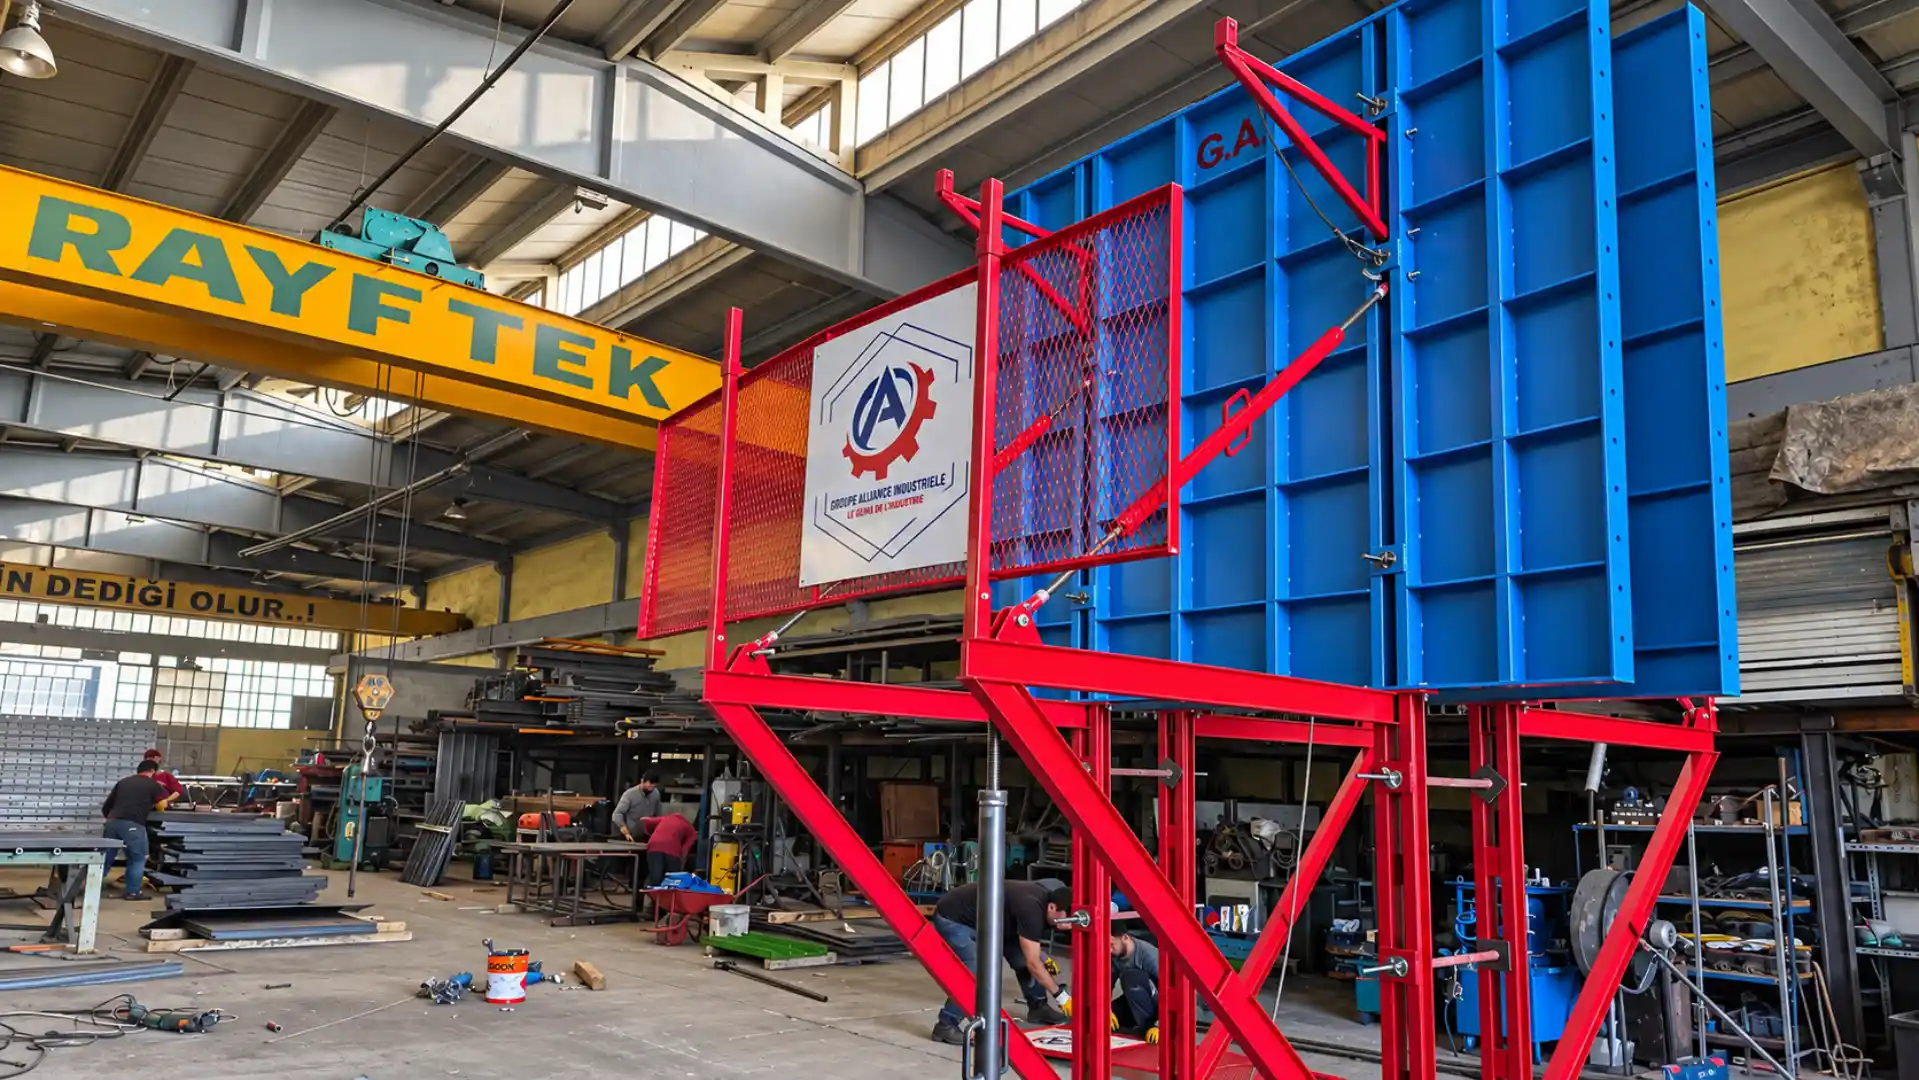
Soma-B Thermal Power Plant
Industrial chimneys are tall structures designed for the controlled discharge of process gases. Wind, seismic action, temperature and maintenance access are all addressed together.
 View Details ↗
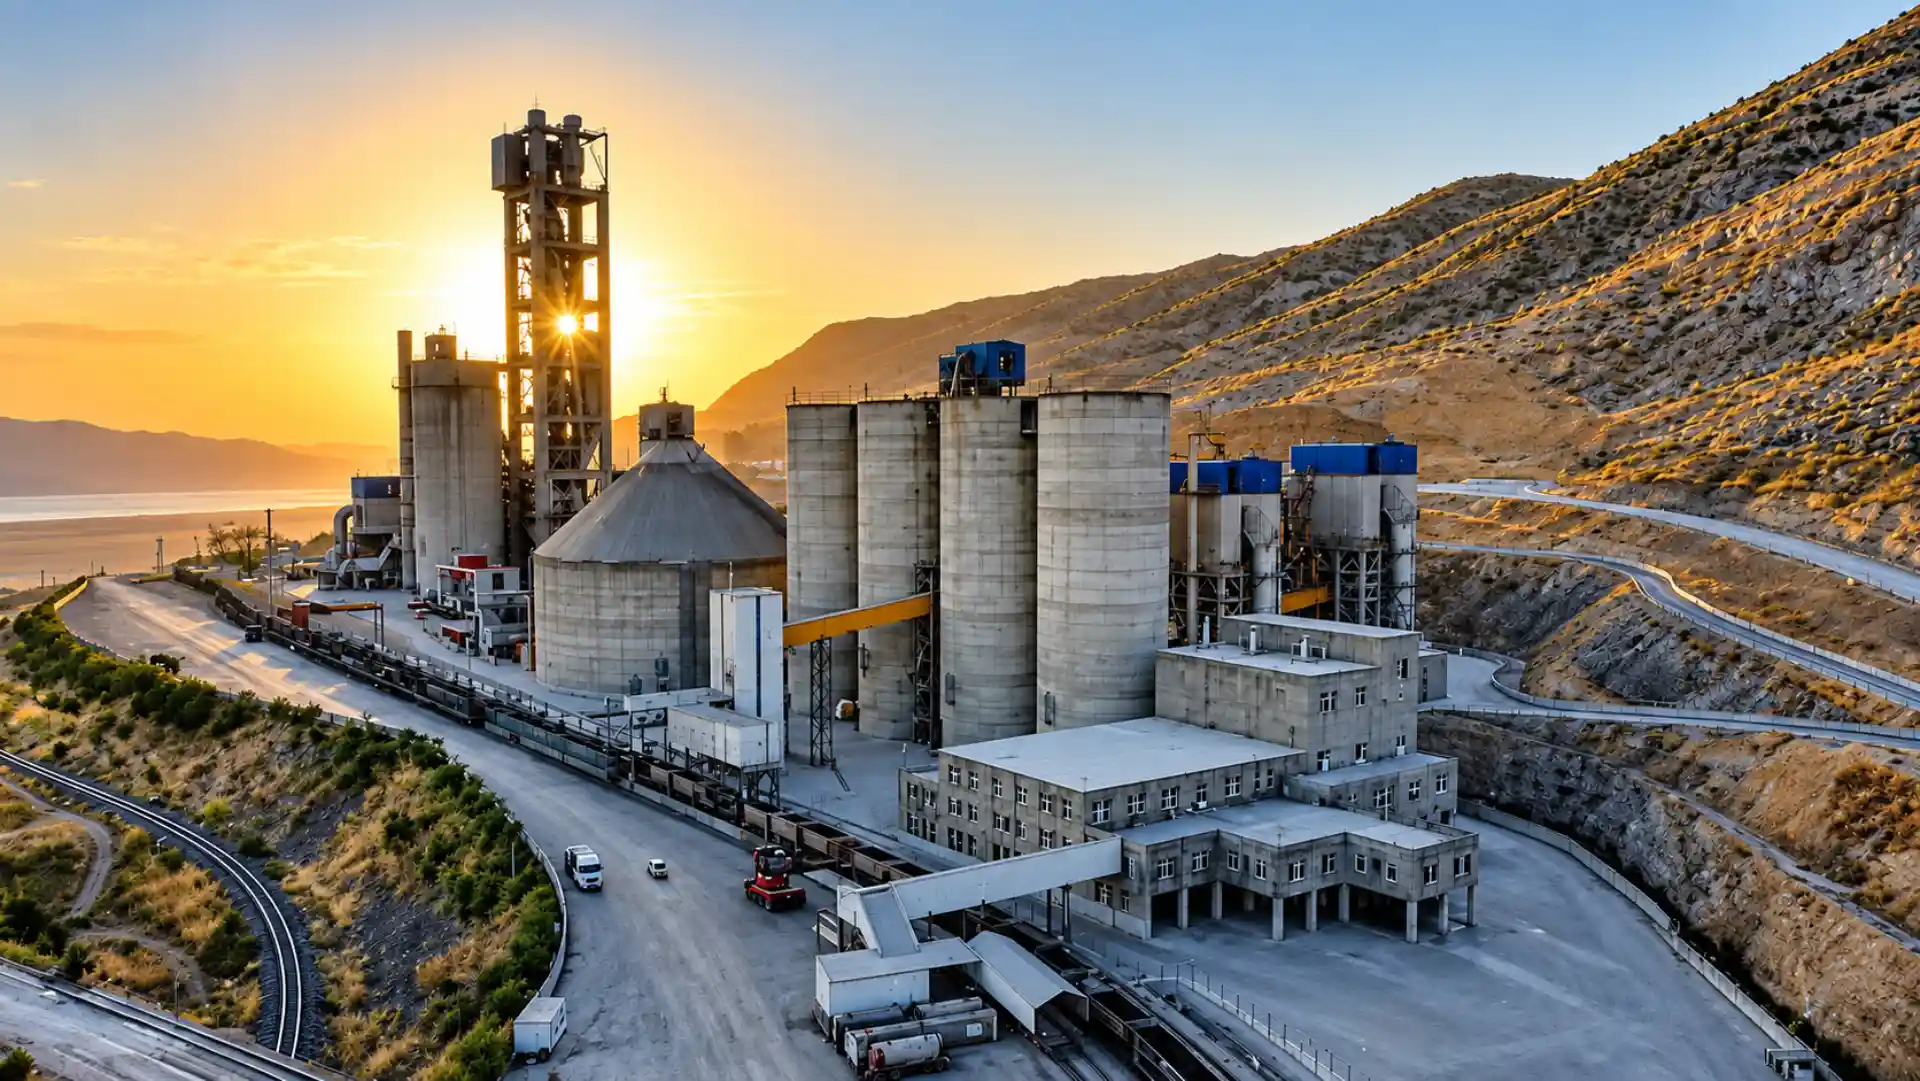
Plain-walled structures of moderate height
Climbing formwork raises tall reinforced-concrete structures in successive concrete lifts. On bridge piers, walls and towers, the formwork is struck and re-erected at the next level.
TECHNICAL SUPPORT
Our technical team will contact you to arrange a gantry or overhead crane site survey and quotation.
Information & FAQ
Short answers on gantry and overhead crane scope, duration and handover.
Gantry cranes, overhead cranes and floor-mounted cranes are all within our fabrication and erection scope. Guided floor-mounted cranes can also be engineered for the maintenance of chimneys and tall structures. The choice of type depends on the span, hoisting class and frequency of use. Girders and trolleys are fabricated in the workshop, while rails and anchorages are installed on site. A load test is carried out before handover and maintenance notes are provided.
A floor-mounted crane limits load sway during chimney maintenance, whereas an overhead crane travels along an enclosed line. Choosing the wrong type puts needless load on the columns. The site survey also checks the roof clearance and escape routes.
The heaviest component to be lifted, load sway, span and duty class are established during the site survey. Girder section, wheels, rails and anchorages are calculated for that load. If future maintenance loads are not taken into account, the crane will soon prove inadequate. The column layout on site can shift the choice between an overhead and a gantry crane. The quotation includes the test load and the control arrangement.
As the duty class increases, fatigue detailing changes. Saying “let's just add a bit of extra capacity” does not automatically upsize the rails and anchorages. The calculation report states the class.
On most hangar and platform projects, rails, anchorages and steel supports are designed to a common site standard. If a crane is added later, the columns and foundations often turn out to be inadequate. That is why the steel drawings and the crane calculations are developed together. The erection sequence also affects painting and electrical routing. At handover, both the structural and the lifting records are kept in the same file.
A crane added as an afterthought catches the roof trusses unprepared. If the two are not designed together, strengthening work follows. This risk may appear as a separate line in the quotation.
Static and dynamic load tests are performed, and brakes, limit switches and rail geometry are checked. Results are recorded in a test report; if there is any deviation, the adjustment is repeated. Critical points are explained to the operator and maintenance team. Spare parts and periodic inspection notes are added to the file. The crane is thus commissioned not as an undocumented machine but as a fully recorded lifting system.
The test load is applied under a different procedure from the nominal catalogue load. Operators must not mistake the test for a production lift. The test report records the witnesses and instrument calibration.